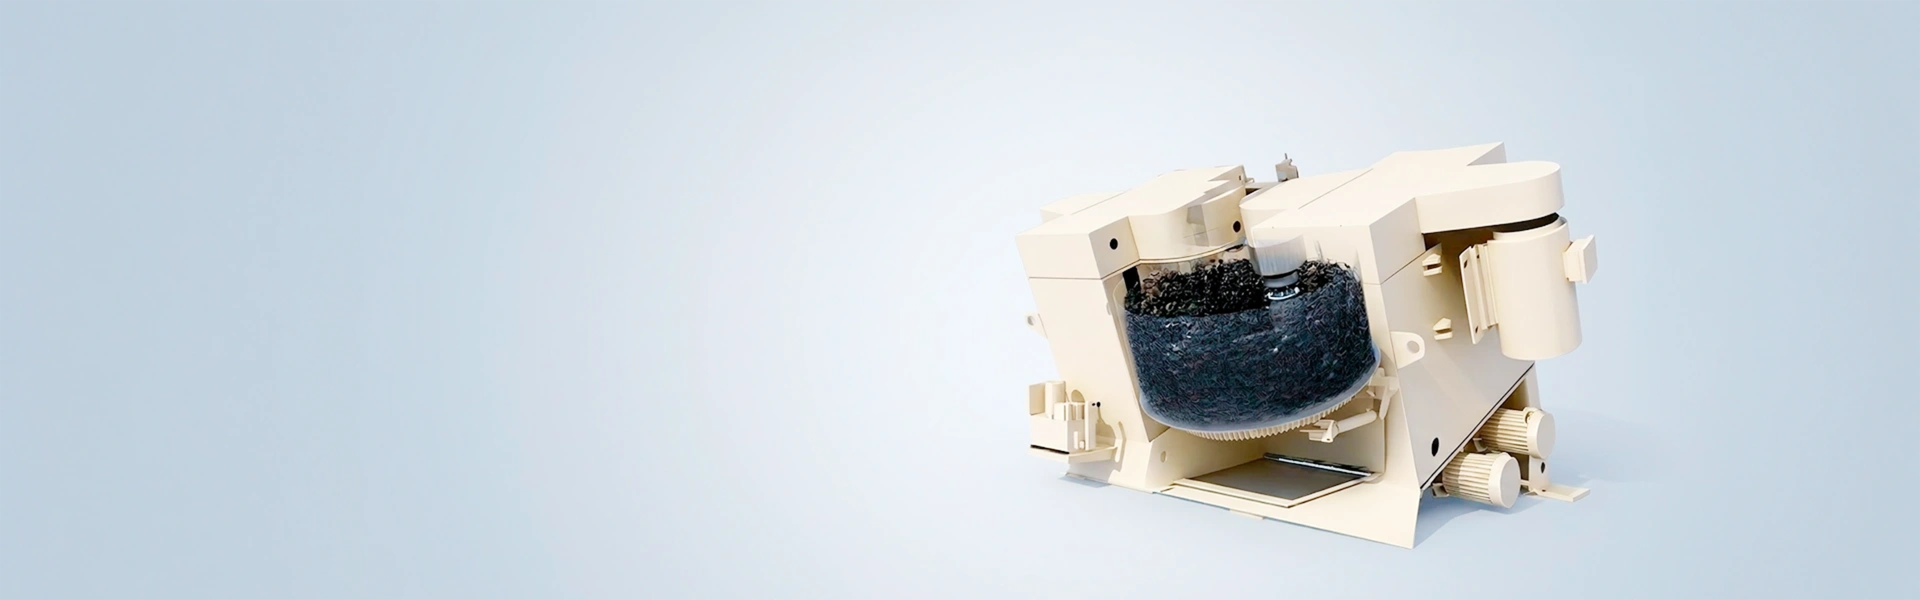
The preparation of foundry sand is the process of pre treating, mixing, and blending the raw sand, binder, and additives according to the process ratio to form qualified molding sand. The foundry sand mixer plays an important role in this process.The core lies in the uniform coating and stable performance of the binder.

Core processes and key controls
1. Raw material pretreatment: New sand needs to be dried to remove impurities and sieved (to remove grass roots, mud lumps, and dust); Old sand needs to be crushed, magnetically separated to remove iron, screened, and cooled (the temperature usually needs to be lowered to below 60 ℃); If clay is raw ore, it needs to be dried and ground into powder, and additives (such as coal powder) need to be crushed and sieved.
2. Mixing process: Adopting the wet to dry or segmented water addition method (first adding sand and some water for initial mixing, then adding clay/powder, and finally adding water for adjustment), using a muller mixer type (high-quality surface sand) or blade type foundry sand mixer(high-efficiency back sand) sand mixer to ensure that the binder evenly wraps around the sand particles; The sand mixing time should be controlled within 3-12 minutes according to the clay content to avoid overheating or uneven mixing.
3. Post processing: After mixing, it is necessary to mix it evenly (for recovery) (let it stand for 2-5 hours to allow water to penetrate and clay to expand) by special foundry sand mixer and loosen the sand (to break up clumps and restore breathability) before it can be used for shaping.
Typical formula reference (taking clay green sand as an example)
• Raw sand/old sand: 100% (basic skeleton, the proportion of old sand is usually higher to reduce costs)
Adhesive: Bentonite 1%~5% (providing wet strength)
• Additional: Coal powder about 3%~8% (anti sticking sand, adjusted according to casting material)
Moisture content: about 3%~6% (precise control of compaction rate and strength)
Key quality indicators:
The prepared molding sand must meet the requirements of wet compression strength, permeability, compactness, and hot wet tensile strength; Modern technology often introduces intelligent systems to automatically monitor moisture and compaction rate and correct them in real-time to ensure batch stability. Special castings (such as resin sand and water glass sand) require specific chemical hardening or regeneration treatment processes